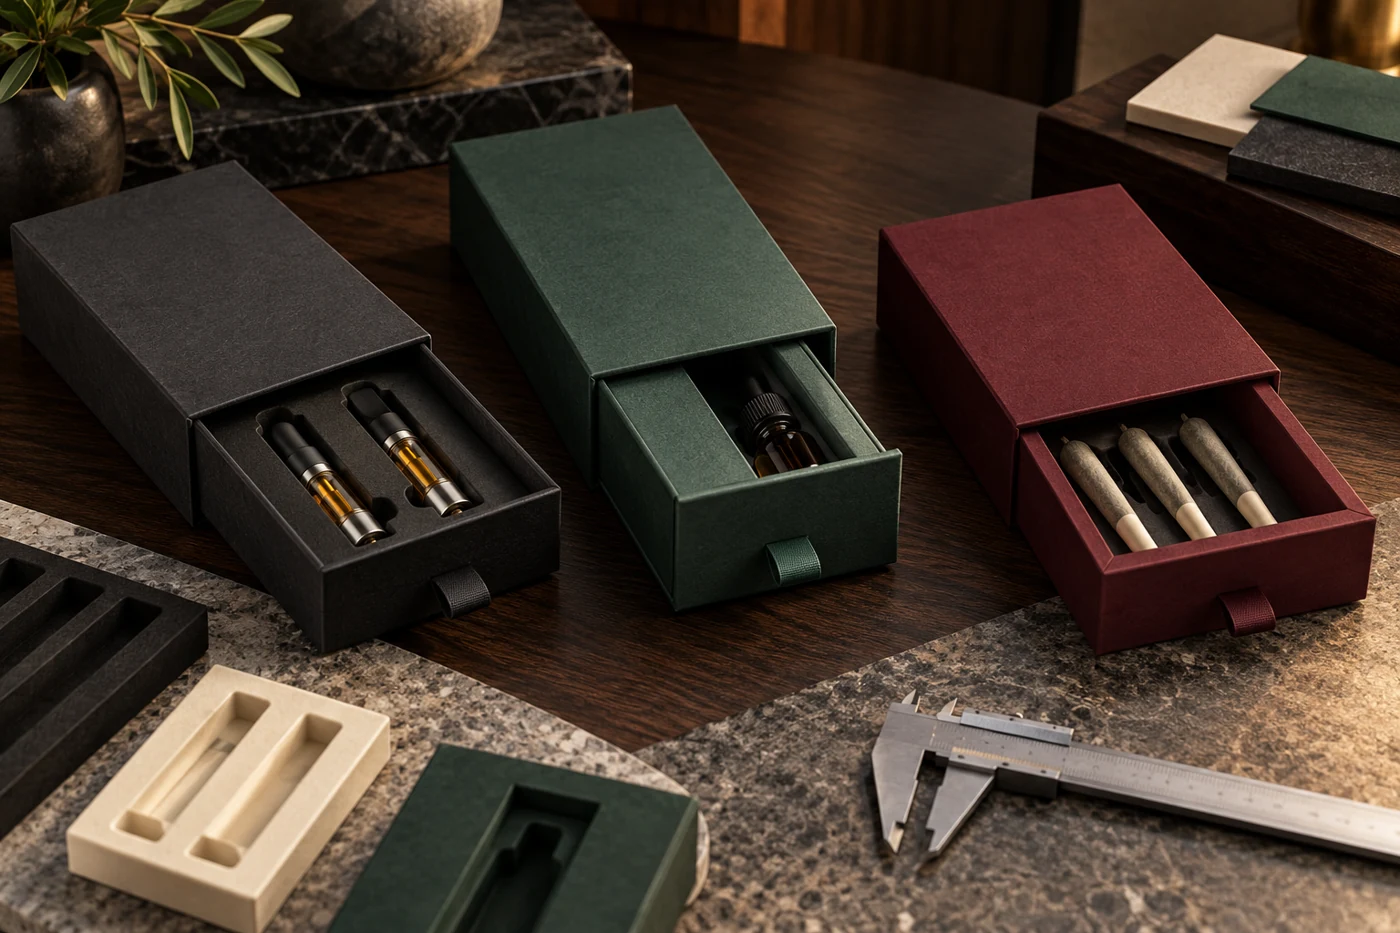
Your drawer boxes usually jam or slide too loosely because the tray-to-sleeve clearance was treated as a single dimension instead of a tolerance system. Greyboard or paperboard caliper, wrap-paper thickness, adhesive, corner build-up, surface finish, insert pressure, product load and storage conditions can all change the final fit. A perfect handmade sample is therefore not enough: buyers need an approved sliding range that can be reproduced across a production batch.
The goal is not the tightest possible drawer. It is a controlled experience: the tray should stay inside the sleeve during normal handling, start moving without excessive force, travel without scraping, and return without catching. This guide shows how to diagnose the failure, set useful specifications and approve a drawer box before mass production.
First identify what “wrong” actually feels like
Do not describe every problem as “too tight.” Observe where the resistance occurs. A tray that binds only at the first few millimetres points to a sleeve-mouth, edge or corner issue. Resistance through the whole stroke suggests insufficient overall clearance, bowing or excessive wrap build-up. A drawer that moves smoothly when empty but jams when loaded suggests insert or product pressure. If the tray rocks sideways or slides out when the box is tilted, clearance or retention is probably excessive.
Record the direction, location and condition of each failure. Test the box level, tilted and after several open-close cycles. Note whether the issue appears on every sample or only part of the batch. That distinction helps separate a design problem from process variation.
Seven variables that control drawer-box fit
1. Tray and sleeve dimensions must include the finished materials
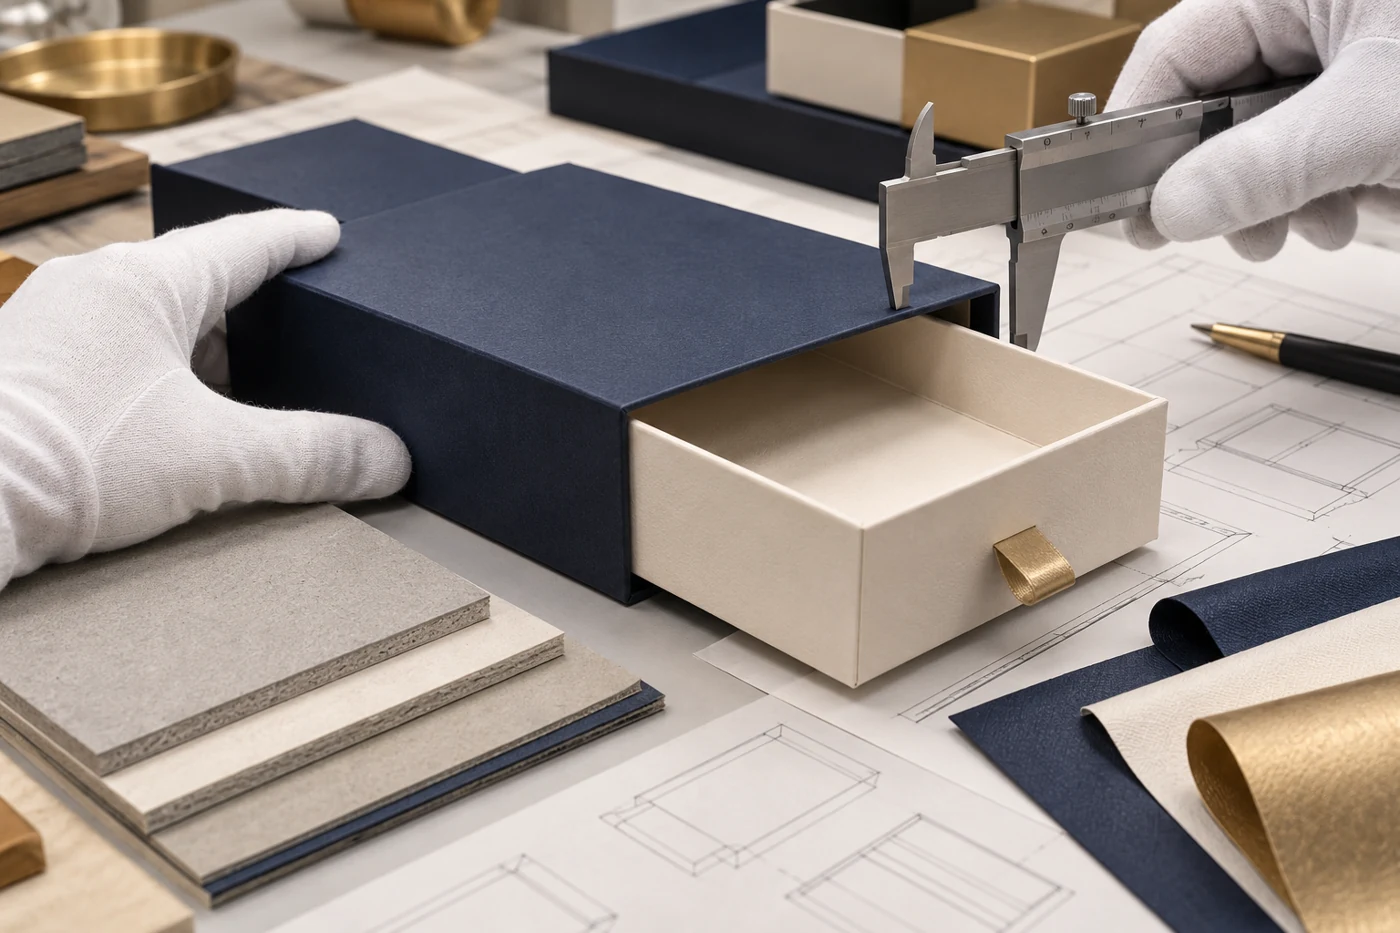
Dieline dimensions alone do not represent the finished box. A rigid tray normally includes board, wrap paper, turned edges and adhesive. The sleeve may include the same layers plus seams or overlapping areas. Every layer occupies space. If the nominal gap is calculated from bare board while the sample is measured after wrapping, the design can lose its intended clearance.
A custom slide-out cartridge box should therefore be specified as a finished system. Ask the supplier to identify the board, wrap and structural dimensions used for both components, and keep the approved construction tied to the dieline revision.
2. Corner build-up can make the tray locally wider
Wrapped corners are rarely identical to a flat wall. Folded paper, adhesive and imperfect turn-ins can create local high points. These points may scrape the sleeve even when average tray width is acceptable. Look for polish marks, compressed fibers or scratches at corresponding corners. If binding occurs at only one corner, increasing the entire gap may create a loose box without solving the workmanship issue.
Inspect corner squareness, wrap overlap and adhesive distribution first. A 510 cartridge drawer package with a long narrow tray is especially sensitive to small angular errors because the tray can enter the sleeve slightly skewed.
3. Board caliper and stiffness affect more than strength
GSM is not a complete fit specification. Two boards with similar basis weight can differ in thickness, density and stiffness. Those differences affect the finished outside dimensions and whether the sleeve stays square. Smurfit Westrock describes its paperboard portfolio in terms of reliable strength and consistent finishes across packaging applications. For a drawer-box buyer, the practical lesson is to approve the actual material grade and thickness range, not only a generic weight description.
Changing board or wrap paper after sampling may change the sliding feel. If substitution is necessary, require a new fit check with the finished structure rather than approving material by appearance alone.
4. Lamination and decorative wraps change surface friction
Fit is both geometric and tactile. An uncoated paper, matte lamination, soft-touch film or textured specialty paper can produce different sliding resistance. Foil, embossing or a seam positioned on a contact face can create a local ridge. A rigid 1 ml cartridge drawer box should be tested with the production surface finish on every sliding area, not with an unfinished white sample only.
Do not try to create a “luxury” feel solely by increasing friction. Controlled resistance can feel premium, but uncontrolled drag makes the product seem defective. Use structure, pull-tab quality, materials and motion together.
5. Inserts and products can distort the tray
An empty tray can pass inspection and still fail after assembly. A tight EVA, paperboard or molded insert may push the sidewalls outward. An oversized bottle cap, cartridge or bundled accessory can do the same. Adhesive used to secure the insert may also introduce local distortion if applied unevenly.
Test the intended product configuration. For a 0.5 ml or 1 ml cartridge package, use the real cartridge, insert and any protective component. Measure the loaded tray and compare its motion with the empty tray. If the loaded version binds, changing only the outer sleeve hides the actual source.
6. Retention features must be separated from sliding clearance
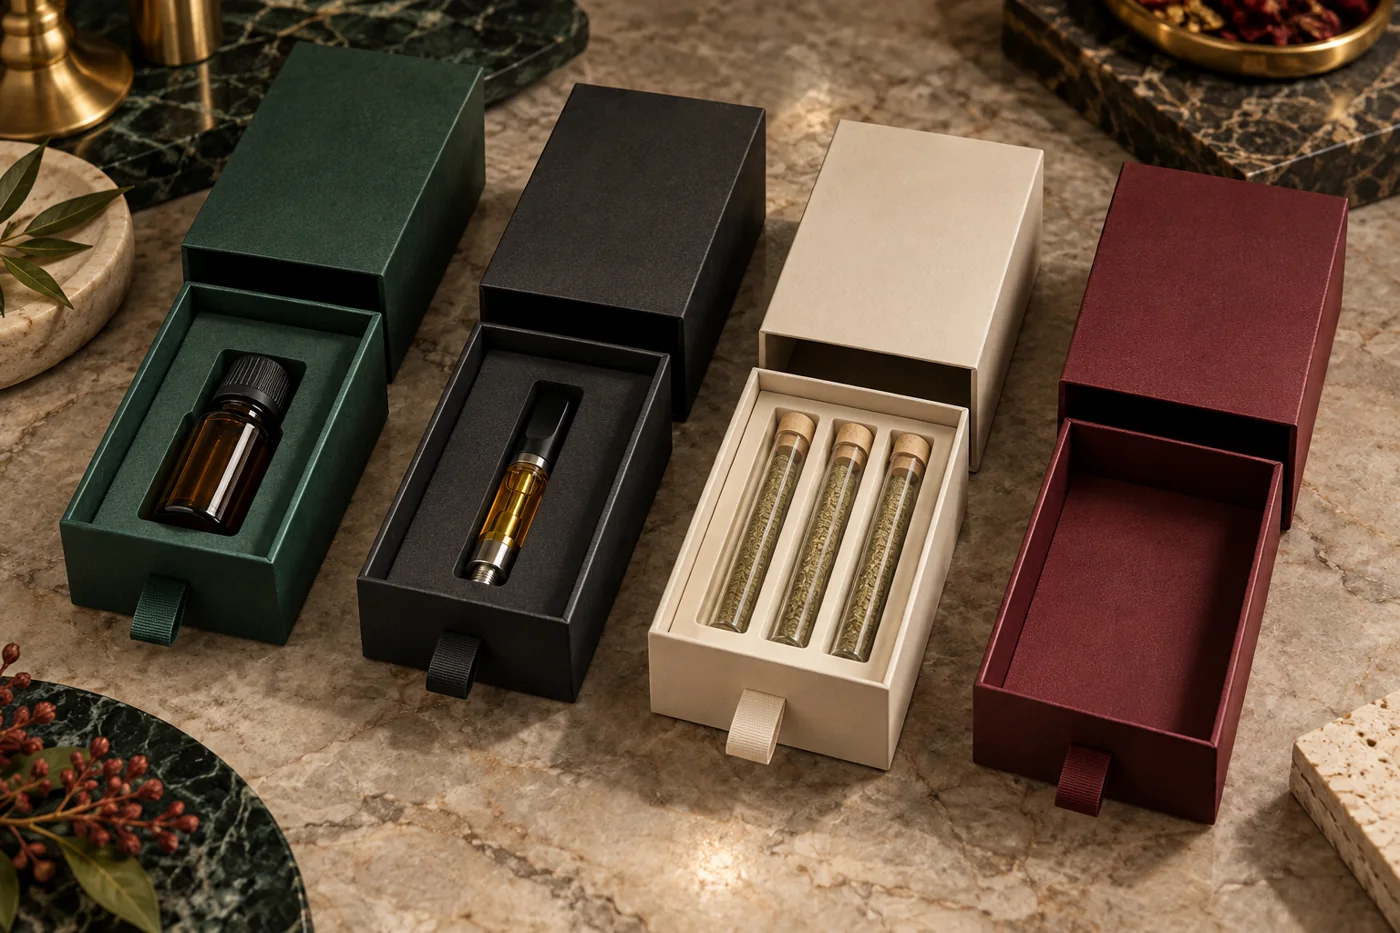
Some drawer boxes need a deliberate stop, lock or child-resistant mechanism. That feature should control opening at a defined point; it should not make the entire travel path unpredictable. A child-resistant pre-roll drawer box needs functional testing of the release mechanism as well as ordinary sliding checks. A child-proof vape cartridge box should also be evaluated with the intended insert and product load.
Do not claim child resistance from appearance or construction alone. Where a regulated child-resistant claim is required, confirm the applicable market requirements and testing route separately. The fit inspection described here does not replace compliance testing.
7. Storage and conditioning can reveal marginal designs
Paper-based components respond to their environment, and a design with almost no tolerance can become unreliable after storage or transport. The objective is not to invent one universal humidity setting. It is to test the finished packaging under conditions relevant to its supply chain and market. Compare samples after normal conditioning, after the expected shipping route and after a reasonable storage period.
Graphic Packaging International’s paperboard information includes products positioned around package integrity and filling-line performance. The broader procurement principle is useful here: material selection should support converting, packing and use—not only print appearance.
Use the failure pattern to choose the next trial
| Observed problem | Likely cause | Controlled trial | Do not do first |
|---|---|---|---|
| Binds only at the sleeve entrance | Mouth distortion, wrap edge or corner build-up | Inspect entrance geometry and corner high points | Increase all clearances |
| Drags through the full stroke | Overall gap, bowing or high-friction finish | Compare finished dimensions and surface combinations | Trim one sample by hand |
| Empty tray works; loaded tray jams | Insert or product expands the tray | Measure and test empty versus fully loaded trays | Enlarge the sleeve only |
| Tray falls out when tilted | Excessive clearance or missing retention | Trial a controlled gap or a defined stop feature | Add random friction points |
| Only some units fail | Process variation, squareness, wrapping or adhesive | Measure samples across the lot and map the failure location | Approve the best sample |
Approve a range, not one perfect sample
Stage 1: confirm the structural direction
Use an undecorated or simply wrapped sample to verify tray depth, sleeve length, product fit, insert design, ribbon position and any stop or release feature. Check whether the tray stays square and whether the product can be removed without pulling the insert out.
Stage 2: test production-intent materials and finishes
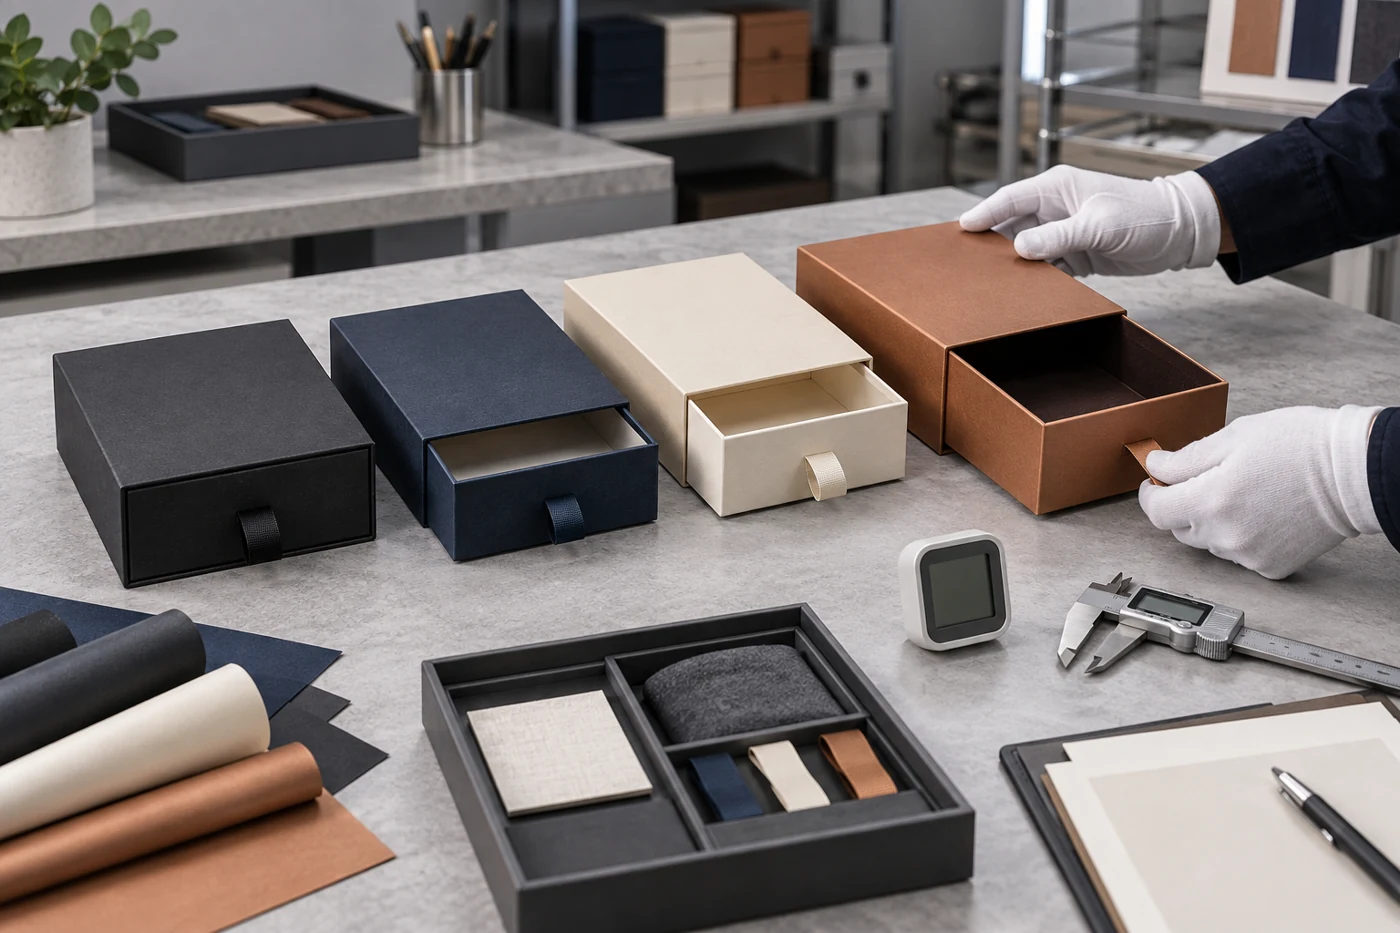
Repeat the sliding check with the approved board, wrap paper, lamination, foil, embossing and adhesive system. Test both empty and fully loaded boxes. Look for rubbing marks and edge damage after repeated operation. Record the accepted feel in practical terms and retain signed limit samples representing the tight and loose boundaries.
Stage 3: inspect a pilot batch
One handmade sample cannot demonstrate process capability. Inspect units from different positions in a pilot batch. Measure finished tray and sleeve dimensions, check squareness and repeat the same tilt, pull and cycle tests. If failures cluster by one corner, one seam or one assembly condition, correct that cause before changing the entire tolerance.
What should a drawer-box RFQ include?
- Finished product dimensions, weight and credible variation.
- Insert material, thickness, cavity layout and retention objective.
- Tray and sleeve material grades, board caliper and wrap specifications.
- Required lamination, textured paper, foil, embossing or other finish in contact areas.
- Desired opening feel, pull-tab style and whether the tray must resist accidental release.
- Any child-resistant or other functional requirement, stated separately from ordinary fit.
- Expected shipping, storage and market conditions.
- Structural sample, finished sample, pilot-batch and limit-sample approval requirements.
When requesting a custom drawer-box review, send the real product and current packaging if possible. A short video showing exactly where the tray catches or how easily it falls out is more useful than the phrase “make it tighter.”
Frequently asked questions
Should a premium drawer box feel tight?
It should feel controlled, not difficult. The appropriate resistance depends on box size, product weight, retention features and user expectations. Define acceptable motion with finished, loaded samples.
Can we fix a loose drawer by using thicker paper?
Possibly, but that changes appearance, friction and dimensions and may create new corner build-up. Diagnose the source and test a controlled revision rather than substituting materials blindly.
Why does the mass-production box feel different from the sample?
Handmade samples, production equipment, material lots, wrapping pressure, adhesive and conditioning can produce different results. That is why production-intent samples and a pilot batch are necessary.
Is one dimensional tolerance enough?
No. Sliding behavior depends on multiple finished dimensions plus squareness, surface friction, corner build-up and loaded-tray distortion. Approve the system and its functional range.
Specify motion as part of the packaging
A drawer box is not successful merely because the tray fits inside the sleeve. Its motion must remain repeatable across materials, finishes, loading and production variation. Define the desired behavior, test the finished loaded pack, keep tight and loose limit samples, and verify a pilot batch. That converts a subjective complaint into a specification the supplier can control.